Executive Summary: Technical Benchmarks of Commercial Grade Ceramics
In the global hospitality supply chain, procuring commercial grade ceramic dinnerware demands a vastly different technical threshold compared to consumer retail tableware. Commercial plates operated within hotels, cruise lines, catering venues, and restaurant groups are subjected to relentless mechanical stress, thermal shock cycles, industrial chemistry, and high-velocity automated washing systems.
As a leading direct manufacturer originating from dedicated production lines (incorporating over 30 years of manufacturing expertise since establishing operations in 1993, backed by a 10,000 square meter standardized facility and 5 million+ pieces annual throughput), our engineering framework adheres strictly to international food contact safety and physical durability metrics:
< 0.2%
Water Absorption Rate
1320°C
High-Temp Firing Kilns
1000+
Wash Cycle Resistance
0.00 %
Lead & Cadmium Release
Understanding Information Gain in ceramic procurement requires analyzing the physical transformation of raw materials during high-temperature vitrification. The inclusion of calcined alumina ($Al_2O_3$) up to 15% to 22% in our proprietary porcelain clay body creates an interlocking mullite crystal matrix. This structural lattice prevents micro-fracture propagation, offering exceptional edge-chip resistance during high-density stacking.
When evaluating ceramic plate manufacturers in China, strategic procurement officers must look beyond initial unit pricing and examine factory infrastructure, raw material stability, quality management systems (QMS), and custom OEM flexibility. ARTWAY has maintained position as a benchmark manufacturer by establishing end-to-end industrial control:
Integrated OEM/ODM Tooling
In-house 3D rapid prototyping and CNC mold production allow bespoke shape development in as little as 7 to 10 working days, reducing NPI lead times by 40%.
Rigorous Compliance
Full compliance with FDA 21 CFR 175.300, California Proposition 65, EU Directive 84/500/EEC, and LFGB standards verified via SGS and Bureau Veritas testing.
Flexible Low MOQ Structure
Standard stock glazed bodies support flexible minimum order quantities, empowering boutique hotel developers and emerging restaurant brands.
Dual Kiln Firing Systems
Utilizing continuous automated roller hearth kilns with digital temperature zone controls to eliminate glaze pinholes and structural warping.
Pre-Shipment Drop-Test QA
Every master carton undergoes ISTA-1A drop testing and thermal shock testing ($\Delta T = 180^\circ C \rightarrow 20^\circ C$) before container sealing.
Technical Comparison: Material Engineering & Durability Profiles
Selecting the correct ceramic substrate is essential for optimizing long-term replacement costs (Total Cost of Ownership - TCO). Below is a quantitative technical matrix comparing standard consumer ceramic bodies against our specialized commercial-grade formulations:
Material Classification
Firing Temperature
Water Absorption Rate
Mohs Hardness (Glaze)
Edge Chip Resistance
Typical HORECA Service Life
Standard Earthenware
1000°C – 1150°C
3.0% – 10.0%
Mohs 4 – 5
Low (Frequent Cracking)
3 – 6 Months
Standard Consumer Stoneware
1200°C – 1250°C
1.0% – 2.0%
Mohs 5 – 6
Moderate
12 – 18 Months
Commercial High-Alumina Porcelain
1300°C – 1340°C
< 0.2% (Fully Vitrified)
Mohs 6.5 – 7
Superior (Rolled Rim)
36 – 60+ Months
Commercial New Bone China
1260°C – 1280°C
< 0.3%
Mohs 6.5
High Flexural Strength
24 – 48 Months
By utilizing high-alumina vitrified porcelain body chemistry, our factory reduces operational replacement rates for hotel food and beverage departments from an industry average of 25% annually to under 5%.
Future Procurement Trends in Commercial Ceramics (2025–2030)
Driven by shifts in global gastronomy, eco-conscious hospitality practices, and supply chain automation, commercial plate sourcing is experiencing rapid technological evolution. Global buyers must align their procurement strategies with four dominant macro trends:
1. Matte Micro-Textured Glazes
Modern culinary presentation has pivoted toward organic, tactile surfaces. Traditional high-gloss glazes are increasingly replaced by matte and semi-matte satin finishes that retain non-porous stain resistance while mitigating silver-marking from heavy cutlery usage.
2. Lightweight Reinforced Geometries
Ergonomic considerations for banquet staff have driven demand for lightweight yet ultra-strong plates. By optimizing finite element wall thickness and reinforcing stress points, plate weight is reduced by 15% without sacrificing mechanical impact thresholds.
3. Sustainable & Low-Carbon Firing
European and North American hospitality brands prioritize suppliers with verifiable ESG credentials. Modern factories are transitioning to natural gas and hydrogen hybrid kilns, coupled with heat-recovery systems that recycle thermal exhaust to pre-dry raw greenware.
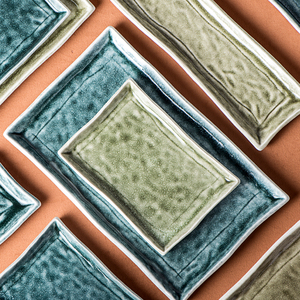
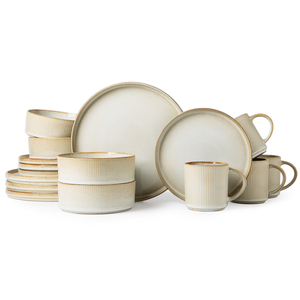
In response to demand for artisan aesthetic appeal combined with industrial performance, our research and development laboratory has introduced specialized reactive glazing technologies. Unlike traditional hand-dipped pottery which suffers from structural instability, our commercial reactive glaze series uses controlled mineral formulations (incorporating iron oxides, titanium dioxide, and cobalt salts) that crystallize during the high-fire soak phase.
Anti-Scratch Zirconium Layer
Glaze formulations enriched with micronized Zirconium Silicate ($ZrSiO_4$) yield a glass surface rated 7 on the Mohs scale, neutralizing metal marking caused by stainless steel 18/10 steak knives.
Anti-Microbial Glaze Additives
Incorporate silver-ion ($Ag^+$) antimicrobial agents into the glaze matrix, inhibiting bacterial cell growth by 99.9% over extended service cycles in healthcare and buffet dining.
Precision Underglaze Decal Firing
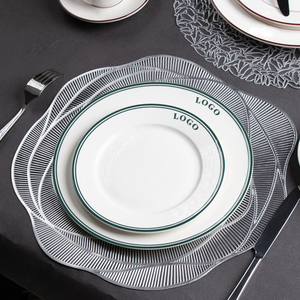
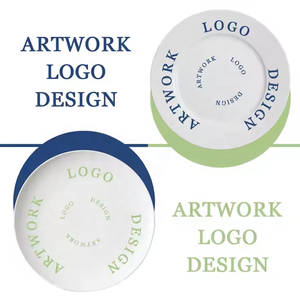
Custom logos and decorative graphics are applied under the protective glaze coat or in-glaze fired at 1250°C, rendering brand graphics completely impervious to acidic foods and alkaline wash chemicals.
Navigating international direct factory procurement involves complex technical questions. Here are detailed responses to the most critical inquiries raised by global procurement executives and importers:
Q:
What is the definitive technical difference between standard domestic plates and commercial grade hotelware?
Commercial hotelware is engineered with calcined alumina for mechanical impact resistance, features a rolled edge design to resist chipping, and undergoes high-temperature vitrification to achieve a water absorption rate under 0.2%. Standard domestic ceramics usually feature higher porosity (>1%) and lack physical rim reinforcement, leading to rapid breakage in industrial dishwashers.
Q:
How does your factory ensure compliance with lead, cadmium, and food contact safety regulations?
Our glazes are 100% lead-free and cadmium-free. We conduct batch-level XRF spectrographic analysis on raw glazes and submit finished products to SGS / Intertek for testing under FDA 21 CFR 175.300, California Proposition 65, European Union Directive 84/500/EEC, and German LFGB standard. Test certificates are furnished with every shipping manifest.
Q:
What are the minimum order quantities (MOQ) and lead times for custom OEM ceramic plate manufacturing?
For standard white glazed bodies with custom logo application, our baseline MOQ starts at 500 to 1,000 pieces per item. For bespoke custom shapes requiring new CNC mold development, MOQ is typically 3,000 pieces. Sample development takes 7 to 10 days, with full container production completed within 30 to 45 days.
Q:
How do you test and guarantee thermal shock resistance for oven-to-table and microwave service?
Our thermal shock testing protocol subjects plates to rapid temperature differentials ($\Delta T = 180^\circ C$). Samples are heated to 200°C in an industrial oven and immediately submerged into 20°C ice-water baths for 5 consecutive cycles. Plates must show zero micro-crazing, cracking, or structural glaze failure to pass quality audit.
Q:
What packaging standards are implemented to guarantee zero breakage during sea freight transport?
We utilize heavy-duty 5-ply corrugated export cartons reinforced with internal EPE foam dividers and corner protectors. Cartons are shrink-wrapped onto fumigated wooden or plastic pallets and strapped securely. Our packaging meets ISTA-1A drop-test standards, guaranteeing container ocean transit break rates below 0.3%.
Q:
Can your factory match pantone colors and custom reactive glazes for private label collections?
Yes, our ceramic color laboratory features automated glaze mixing technology capable of precise Pantone color matching. For reactive glaze collections, we establish control range boundaries (master samples showing high/low color variance tolerance) to ensure batch consistency across mass production runs.
Partner with China's Premier Commercial Ceramic Manufacturer
Streamline your supply chain with direct factory pricing, certified food contact safety, and industry-leading rim durability. Contact our B2B engineering team today for technical catalogs, instant FOB quotes, and physical sample requests.